


HT601P-2
2-Laser SLS for Large Parts
Farsoon HT601P-2 features a 600 × 600 × 600 mm build volume and 2 x 100 W CO₂ lasers with a dynamic-focus digital galvo system. Top loading with bottom feeding, multi-zone thermal control, and an open platform make it well suited to large industrial components and dense batches.
Browse Farsoon 3D printers.
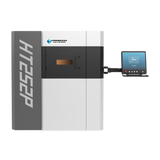
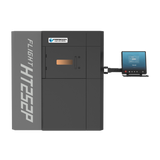

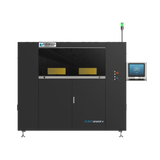



The products below are optional but included in the quote for successful operation.
Equipment: MCWI-70C Chiller, FS601P.T16 Powder Feeding Unit, FS-PBS-601P Powder Cleaning Station, NPM-V150 Powder Mixer, ATTIX 961-01 Industrial Vacuum Cleaner, HC-1580a-2 Sandblasting Machine, HSFD39-5 Nitrogen Generator, LG-10 Air Compressor


Technical Specifications
Download DatasheetSLS (Selective Laser Sintering)
600 × 600 × 600 mm
2 × 100 W CO₂ Laser
High-Precision 3-Axis Galvanometer System
≤ 20 m/s
220 °C
0.06–0.30 mm
Nitrogen
Multi-Zone Heater and Intelligent Temperature Control Systems
Real-Time, Continuous Monitoring and Optimization of the Build Surface Temperature
Windows 11 (64-Bit)
BuildStar, MakeStar®: Open Access to Core Machine Parameters, Real-Time Changes to Build Parameters, 3D Visualization and Fault Diagnostics
STL
1,862 × 1,832 × 2,350 mm
~ 3,300 kg
400 V ±10%, 3~/N/PE, 50/60 Hz, 60 A
22–28 °C
CE
FS1088A-TPU (TPU), FS1092A-TPU (TPU), FS3150CF (PA12-CF), FS3250MF (PA12-MF), FS3300PA (PA12), FS3401GB (PA12-GB), FS4100PA (PA11), FS6140GF (PA6-GF), FS3201PA-F (PA12), FS3300PA-F (PA12), FS3401GB-F (PA12-GB), FS6130CF-F (PA6-CF)
The system is an open platform; besides the listed materials, it is also compatible with third-party materials that the machine specifications support. Parameters must be developed separately.
2-Laser Production for Large Parts
A 2-laser CO₂ platform with a 216-liter build volume, for large industrial components and dense batches.

Top Loading, Bottom Feeding
A new powder feeding method gives dense, homogeneous spreading with less streaking and fewer layer defects.

Dynamic Focus Digital Galvo
Constant spot size and energy density across the 600 mm optical field, with ±3 °C chamber uniformity.

Smart Production Line
Unattended production with a powder management system (PMS), automatic cartridge transfer and controlled cooling.

Air Duct
A key component that provides controlled airflow in the vehicle. Conventional methods can only make the large, complex hollow structure in several pieces, while SLS produces it as a single part.
- Material
- FS3300PA (PA12)
- System
- HT601P-2
System Workflow
-
Data Preparation
The build is laid out in BuildStar.
-
Powder Feeding
Powder is fed automatically from the top.
-
3D Printing
Parts are built layer by layer with the laser.
-
Cartridge Transfer
The cartridge is moved to cooling on the cartridge cart.
-
Depowdering
Parts are removed at the station.
-
Post-Processing
Sandblasting and surface finishing are applied.


