


403P Series
High-Throughput SLS Platform
Farsoon 403P Series is a configurable, high-performance SLS system designed for everything from cost-efficient prototyping to full-scale production. Advanced temperature shielding, laser power, and thermal control ensure stable processing and high part quality.
Browse Farsoon 3D printers.
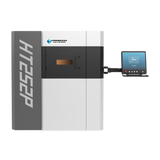
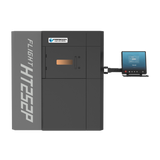




The products below are optional but included in the quote for successful operation.
Equipment: MCWI-15C Chiller, FS-EC-01P External Cooling Station, FS04-PPS Powder Cleaning Station, FS-PMS-02P Powder Management System, FS-M-50 Powder Mixer, ATTIX 961-01 Industrial Vacuum Cleaner, HC-9060A Sandblasting Machine, HSFD39-5 Nitrogen Generator, LG-10 Air Compressor, DHG-9123AS Powder Drying Oven


Technical Specifications
Download DatasheetSLS (Selective Laser Sintering)
400 × 400 × 540 mm
HS403P-H: 1 × 55 W CO₂ Laser
SS403P-H: 1 × 100 W CO₂ Laser
HT403P-H: 1 × 100 W CO₂ Laser
High-Precision 3-Axis Galvanometer System
≤ 20 m/s
HS403P-H: 190 °C
SS403P-H: 190 °C
HT403P-H: 220 °C
0.06–0.30 mm
Nitrogen
Eight-Zone Heater and Intelligent Temperature Control Systems
Real-Time, Continuous Monitoring and Optimization of the Build Surface Temperature
Windows 11 (64-Bit)
BuildStar, MakeStar®: Open Access to Core Machine Parameters, Real-Time Changes to Build Parameters, 3D Visualization and Fault Diagnostics
STL
2,540 × 1,370 × 2,225 mm
~ 3,000 kg
400 V ±10%, 3~/N/PE, 50/60 Hz, 32 A
22–28 °C
CE
HS403P-H and SS403P-H: FS1088A-TPU (TPU), FS1092A-TPU (TPU), FS3150CF (PA12-CF), FS3250MF (PA12-MF), FS3300PA (PA12), FS3401GB (PA12-GB), FS4100PA (PA11), FS3201PA-F (PA12), FS3300PA-F (PA12), FS3401GB-F (PA12-GB)
HT403P-H: FS1088A-TPU (TPU), FS1092A-TPU (TPU), FS3150CF (PA12-CF), FS3250MF (PA12-MF), FS3300PA (PA12), FS3401GB (PA12-GB), FS4100PA (PA11), FS6140GF (PA6-GF), FS3201PA-F (PA12), FS3300PA-F (PA12), FS3401GB-F (PA12-GB), FS6130CF-F (PA6-CF)
The system is an open platform; besides the listed materials, it is also compatible with third-party materials that the machine specifications support. Parameters must be developed separately.
Exchangeable Cartridges for Uninterrupted Workflow
Farsoon’s flagship polymer production system: exchangeable build and feed cartridges, external cooling and powder management for an uninterrupted workflow.

Precise and Repeatable
An eight-zone heater and intelligent thermal control mean less deformation and higher dimensional accuracy.

High-Temperature Configuration
With its 220 °C chamber, the HT403P-H processes high-performance materials such as PA6 into direct-use parts.

Exchangeable Cartridges
The cartridge is swapped as soon as the build finishes; cooling continues outside the machine in an inert atmosphere, so downtime is kept to a minimum.

Custom Lens Antennas
A Luneburg lens design: a multilayer structure in an extremely compact volume, with variable layer thickness and many fine details for different electromagnetic wave refraction.
- Material
- FS3300PA (PA12)
- System
- HT403P-H
System Workflow
-
Data Preparation
The build is laid out in BuildStar.
-
Cartridge Loading
Powder is filled into the feed cartridge.
-
3D Printing
Parts are built layer by layer with the laser.
-
Cartridge Change
The cartridge cools outside the machine.
-
Depowdering
Parts are removed at the station.
-
Post-Processing
Sandblasting and surface finishing are applied.


