


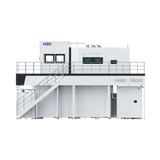
HBD 1600
Aerospace-Grade Production with 28 Lasers
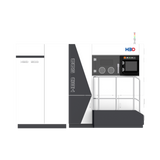
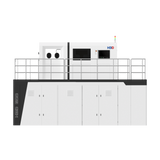
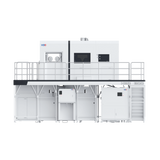
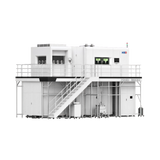
HBD 1600 reaches a build rate of 840 cm³/h with 28 high-precision lasers across a 1600 × 1600 × 1750 mm build volume. Automatic blade replacement, self-cleaning lenses, and closed-loop powder circulation let it produce rocket-engine-scale aerospace parts in a single build.


Technical Specifications
Download DatasheetLPBF (Laser Powder Bed Fusion)
1,600 × 1,600 × 1,750 mm (Height Including Build Plate)
20–120 µm
28 × 500 W Maxphotonics Laser; 28 × 1,000 W Maxphotonics Laser; 28 × 500 W IPG Photonics Laser; 28 × 1,000 W IPG Photonics Laser
≤ 10 m/s
70–200 µm
≤ 100 ppm
Fully Sealed Chamber; Automatic Oxygen Monitoring, Recirculating Purification and a Collection Coefficient of ≥ 99%
> 99.9%
0.05–0.2 mm
840 cm³/h
Blade wear is monitored in real time; a redundant dual-blade design allows fully automatic blade changes.
Lens Self-Cleaning System
Closed-Loop Powder Circulation; Automatic Recycling, Sieving and Feeding
Application-Specific Parameter Set; User-Editable
HBD AMES – HBD System Machine Control Software and HBD Build Expert Path-Planning Software; Open Parameter Structure
STL
12,500 × 5,920 × 7,500 mm
~ 71,500 kg
500 W: AC 380 V, 50 Hz, Peak Power 50 kW, Average Power 25 kW
HBD 316L (Stainless Steel), HBD 15-5PH (Stainless Steel), HBD 17-4PH (Stainless Steel), HBD 18Ni300 (Maraging Steel), HBD 420 (Tool Steel), HBD CX (Tool Steel), HBD AlSi10Mg (Aluminum Alloy), HBD TC4 (Titanium Alloy), HBD TA15 (Titanium Alloy), HBD CoCrMo (Cobalt Alloy), HBD IN718 (Superalloy), HBD IN625 (Superalloy), HBD Hastelloy X (Superalloy), HBD GH99 (Superalloy), HBD GH230 (Superalloy)
The system is an open platform; besides the listed materials, it is also compatible with third-party materials that the machine specifications support. Parameters must be developed separately.
Aerospace-Grade Production: 28 Lasers
With a 1,600 × 1,600 × 1,750 mm build volume and 28 high-precision lasers, the HBD 1600 produces rocket-engine-scale parts in a single build, with a build rate of 840 cm³/h, automatic blade changes and closed-loop powder circulation.
Automatic Blade Change System
Blade wear is monitored in real time and blades are changed fully automatically; a redundant dual-blade design supports long, uninterrupted builds.

Lens Self-Cleaning System
Dust is cleaned from the lens automatically, preventing optical path attenuation and reducing lens-maintenance downtime and long-term operating costs.

Closed-Loop Powder Circulation
Automatic recycling, sieving and powder feeding during printing reduce manual intervention and improve powder utilization and operational safety.

High-Efficiency Multi-Laser Source
28 High-precision lasers and the HBD galvanometer system reach a build rate of 840 cm³/h, significantly shortening part lead times.

3D printed with HBD 1600.

Exhaust Diffuser

Large Turbine Blade

Sectioned Housing

Suspension Node Bracket

Turbine Blade Set
From powder to finished part in twelve steps.
The entire process runs on a single line with HBD equipment and additional modules.
-
Powder Drying
-
3D Print Preparation
-
Sieving and Suction
-
Powder Feeding
-
3D Printing
-
Depowdering
-
Stress Relief
-
Removal from the Build Plate
-
Support Removal
-
Heat Treatment
-
Sandblasting
-
Grinding


